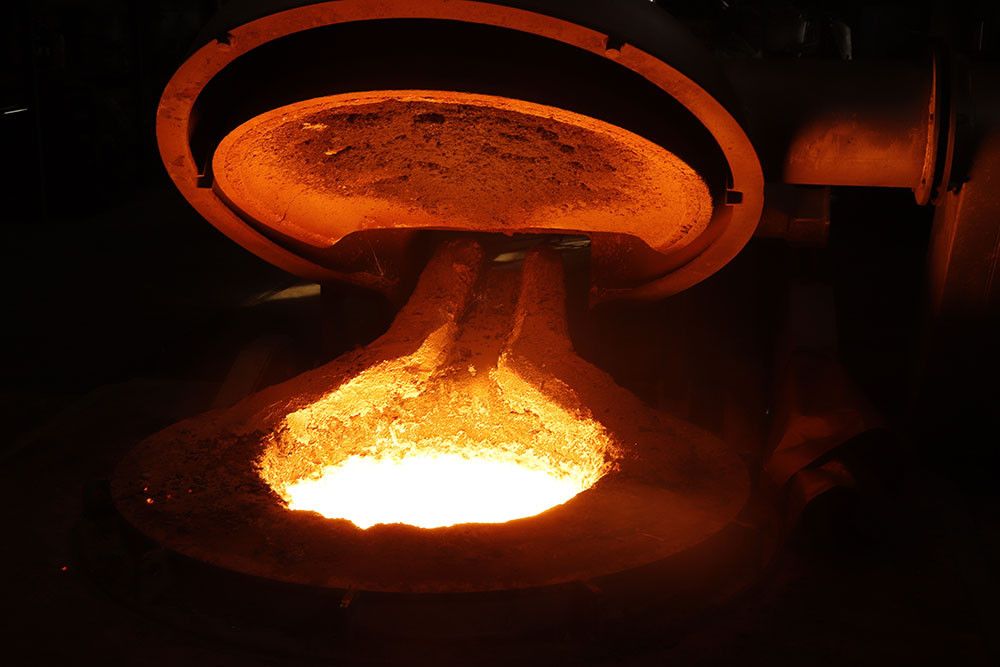
01 — Melting
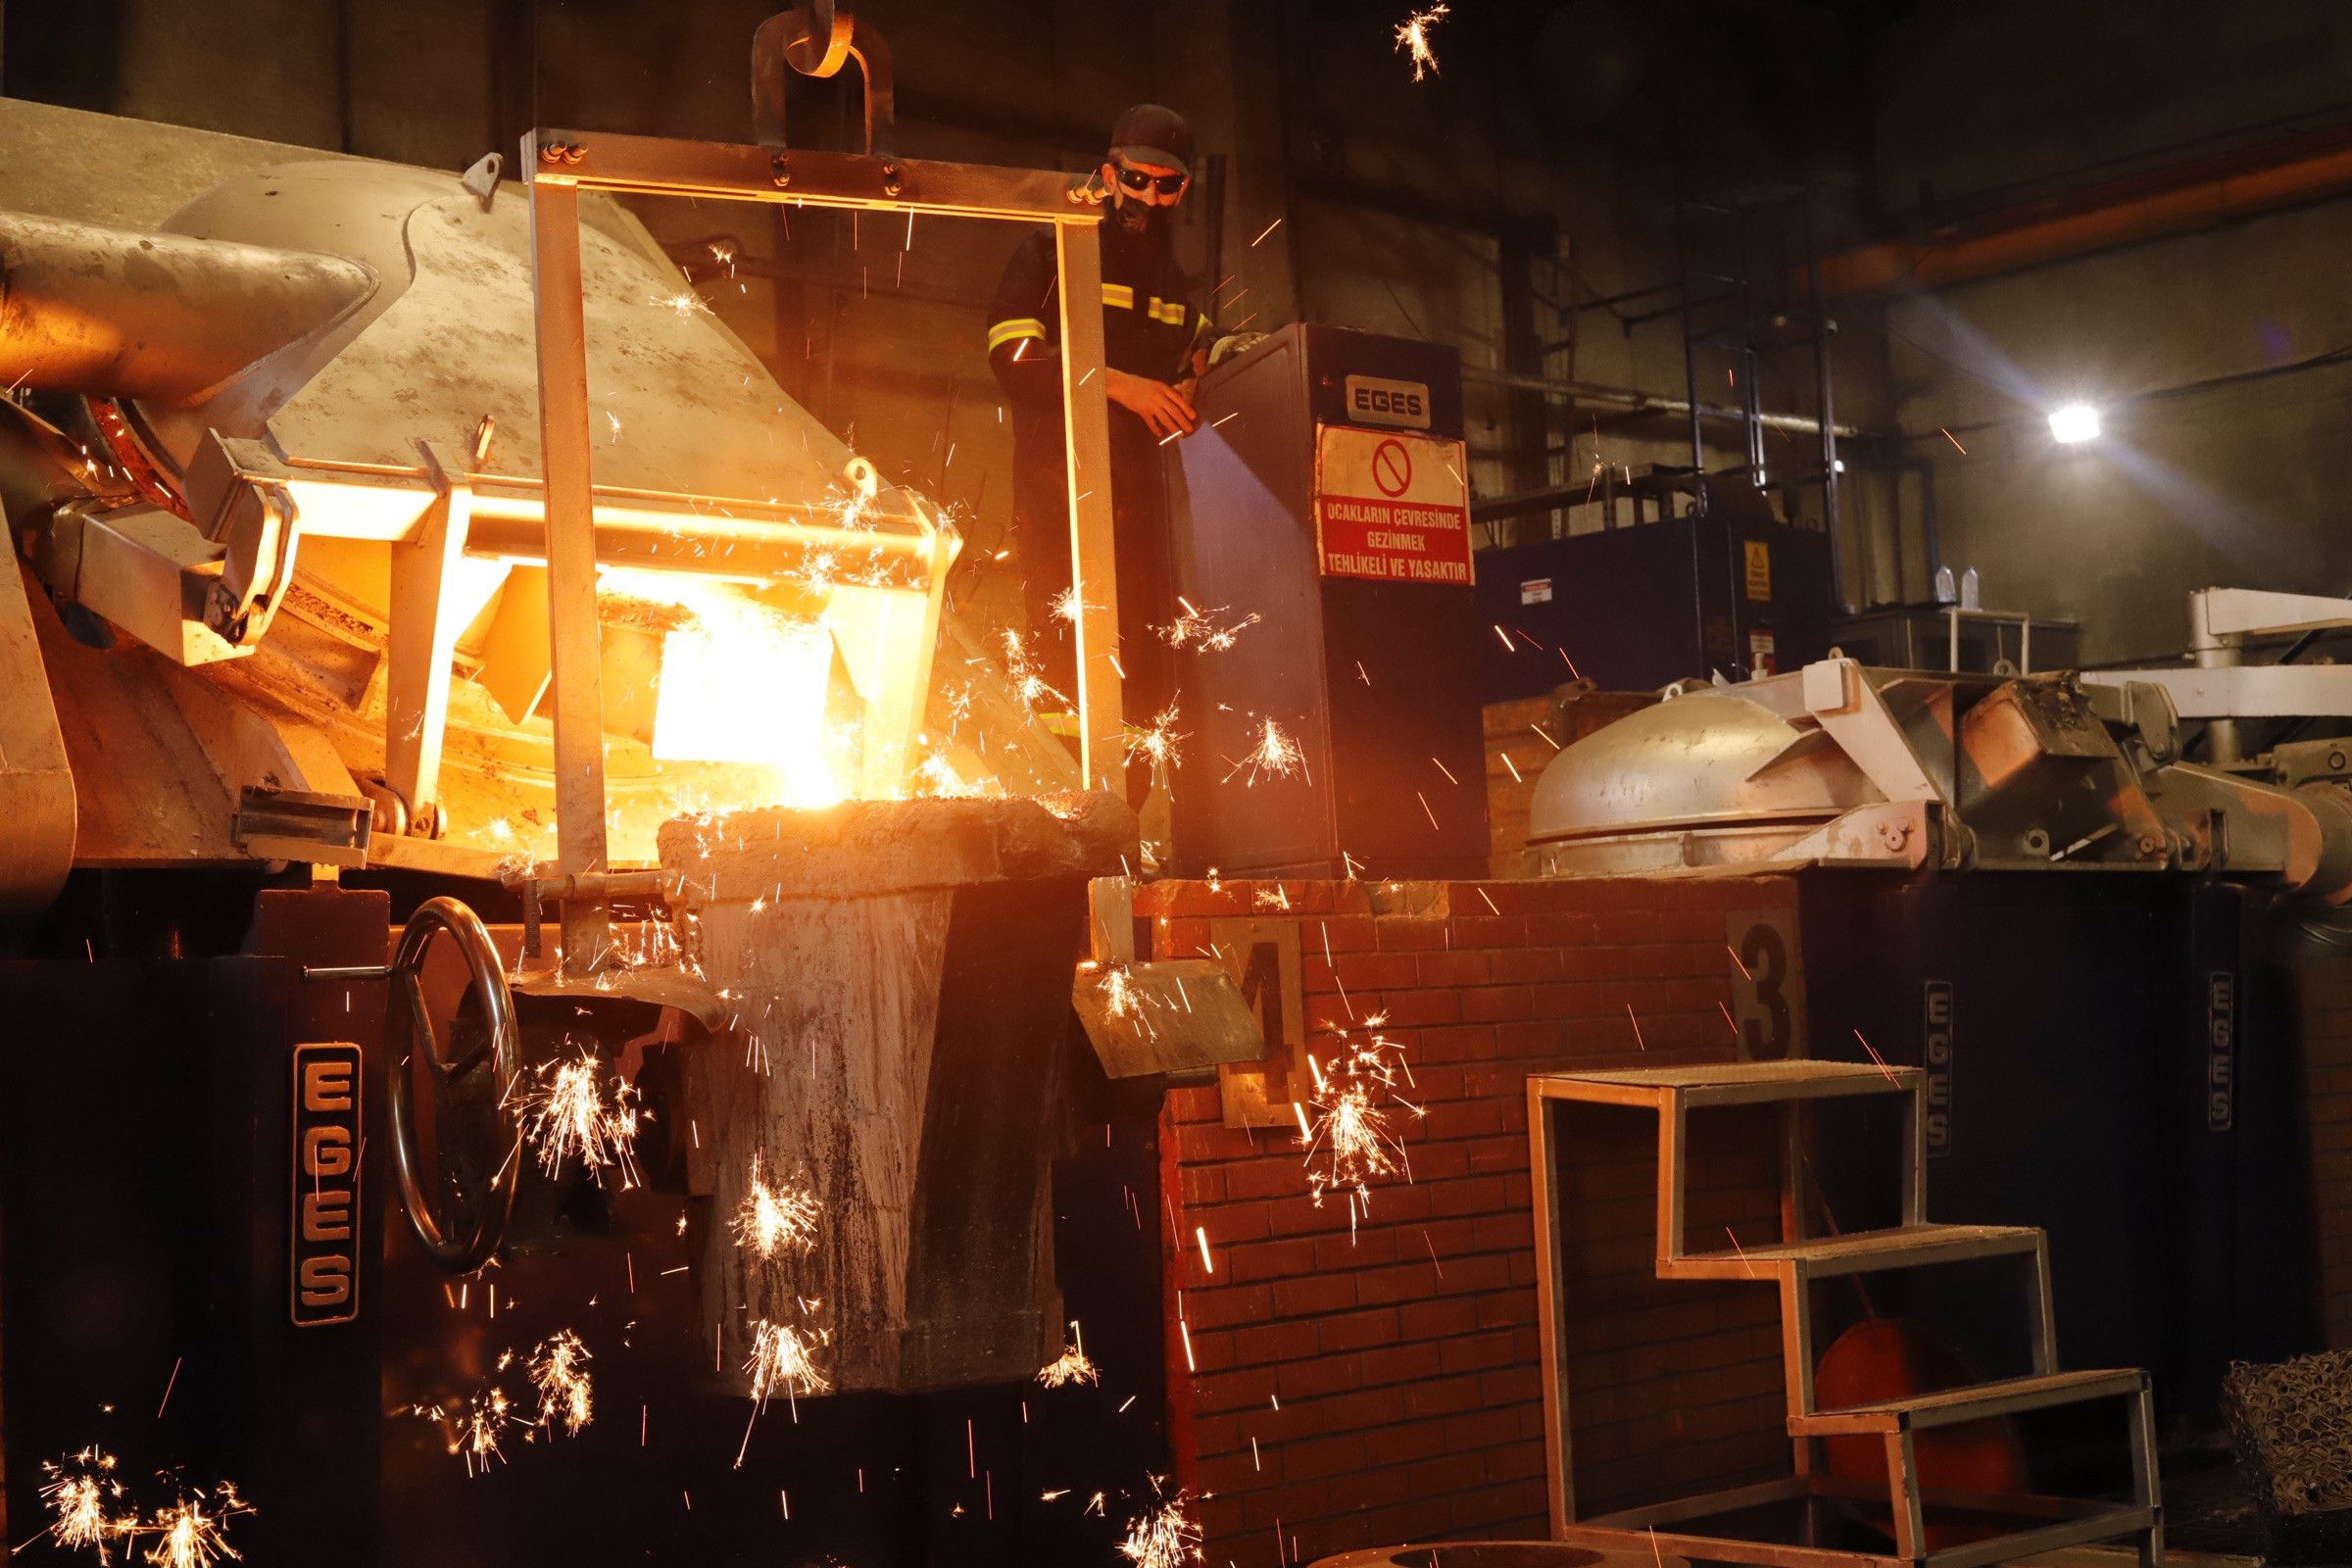
4 induction furnaces
2 × 2.5 t Eges (dual-track) and 2 × 1.5 t Inductotherm (power-track).
01 — End-to-end process
These are the stages of the casting process; you can open the detail page for each of them.
/ 01
Pattern and mould work is carried out with 3D modelling programs such as Solidworks.
/ 02
Magmasoft simulation is used for casting efficiency.
/ 03
Cold-box and hot-box cores are produced with an automatic sand preparation system.
/ 04
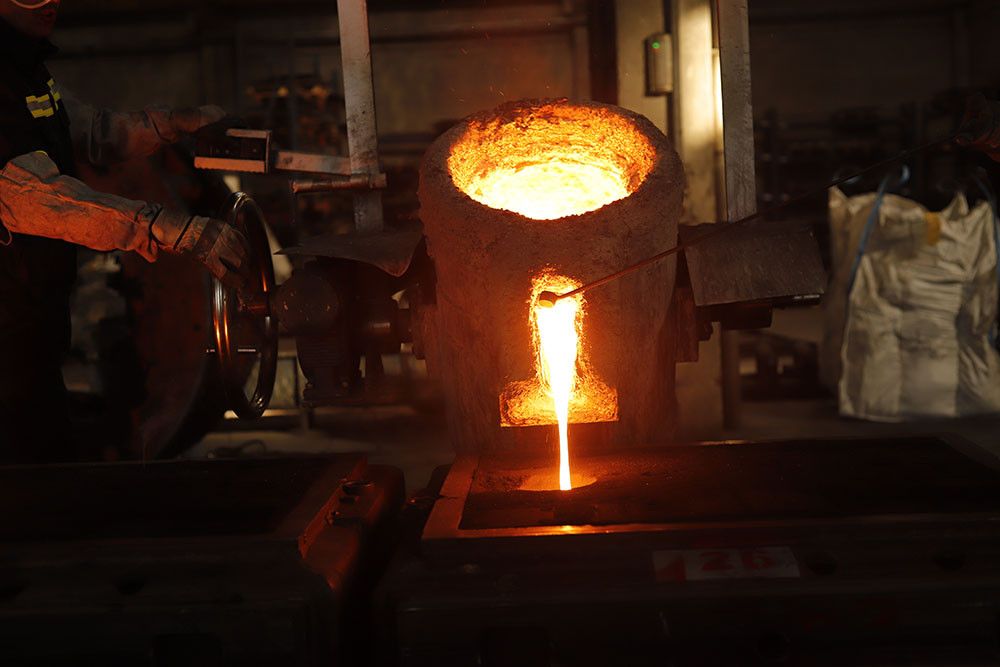
Melting in induction furnaces; Disamatic vertical moulding, horizontal flask moulding and centrifugal casting.
/ 05
Horizontal and vertical lathes with C and Y axes, vertical machining centres and precision indexing horizontal machining centres.
/ 06
Cataphoretic coating and liquid paint for parts of various sizes; wet enamel plant.
/ 07
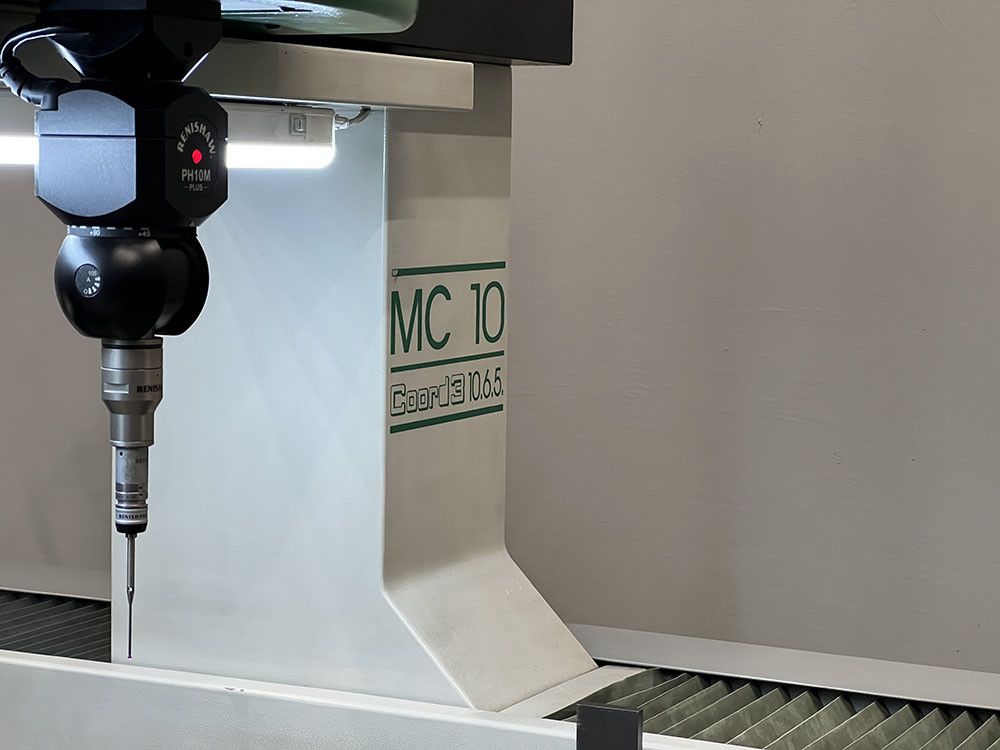
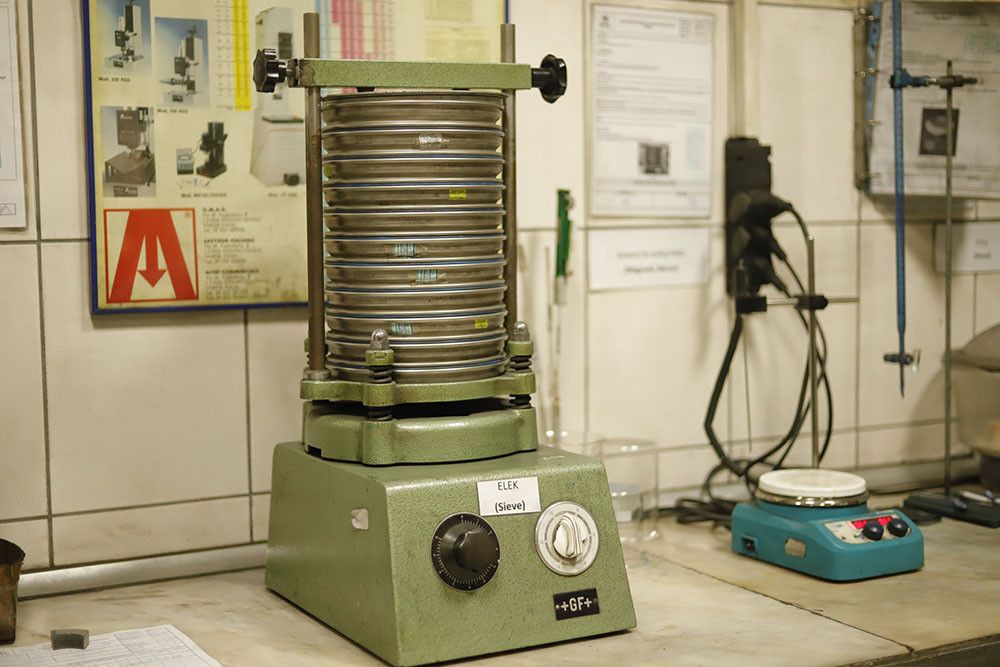
Sand, metallurgical, metallographic, precision dimensional measurement and coating quality checks.
02 — Engineering support
The pattern shop uses 3D modelling programs such as Solidworks. On the casting side, Magmasoft simulation is used.
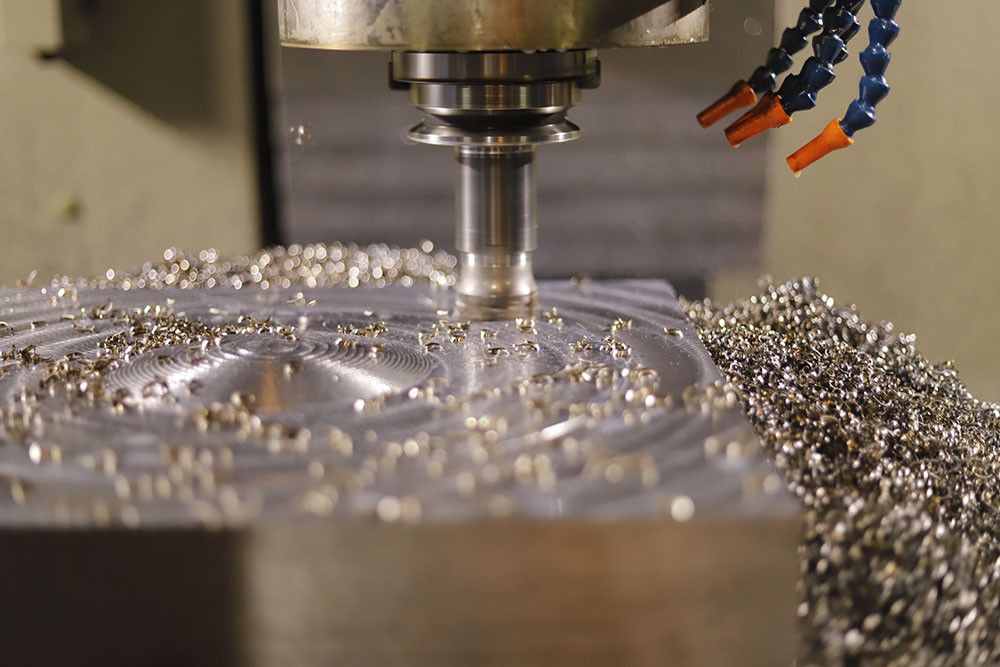
03 — Production infrastructure
The main equipment and technologies used from melting to coating.
2 × 2.5 t Eges (dual-track) and 2 × 1.5 t Inductotherm (power-track).
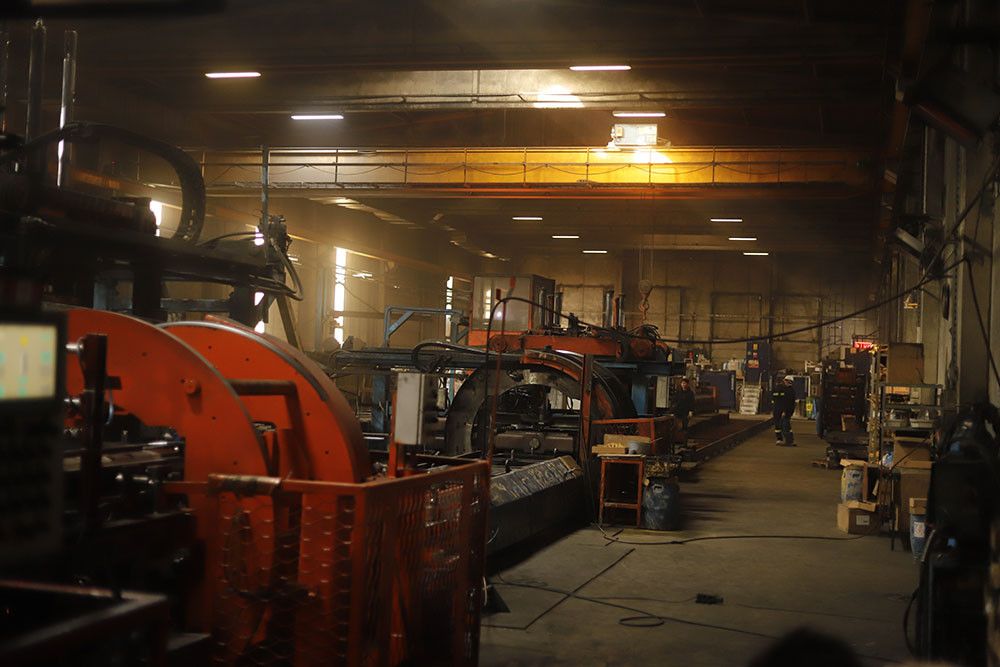
Disamatic vertical moulding, horizontal flask moulding and centrifugal casting.
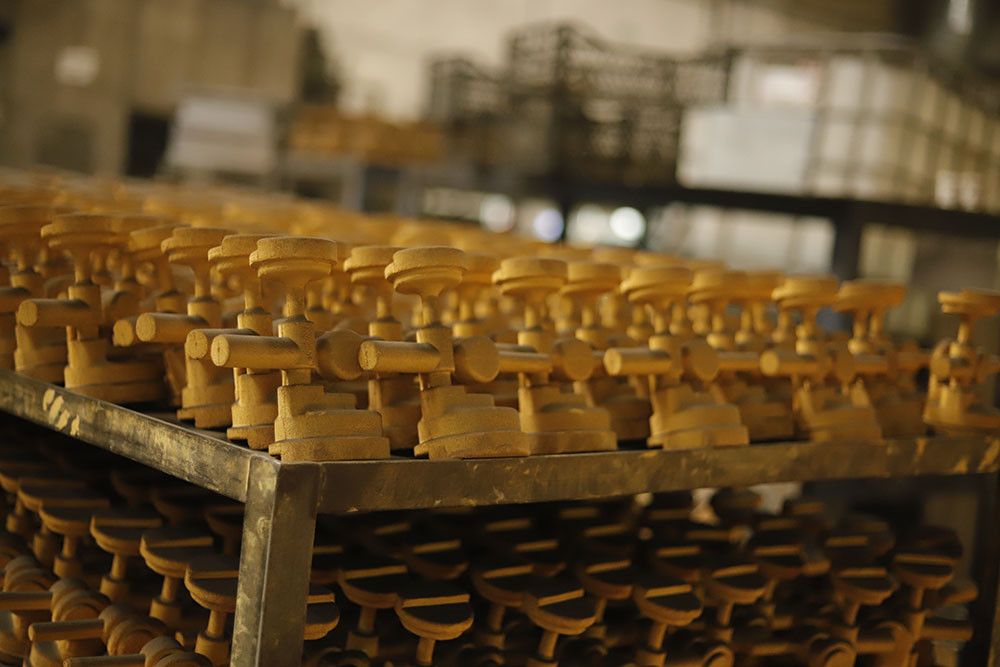
Automatic sand preparation system.
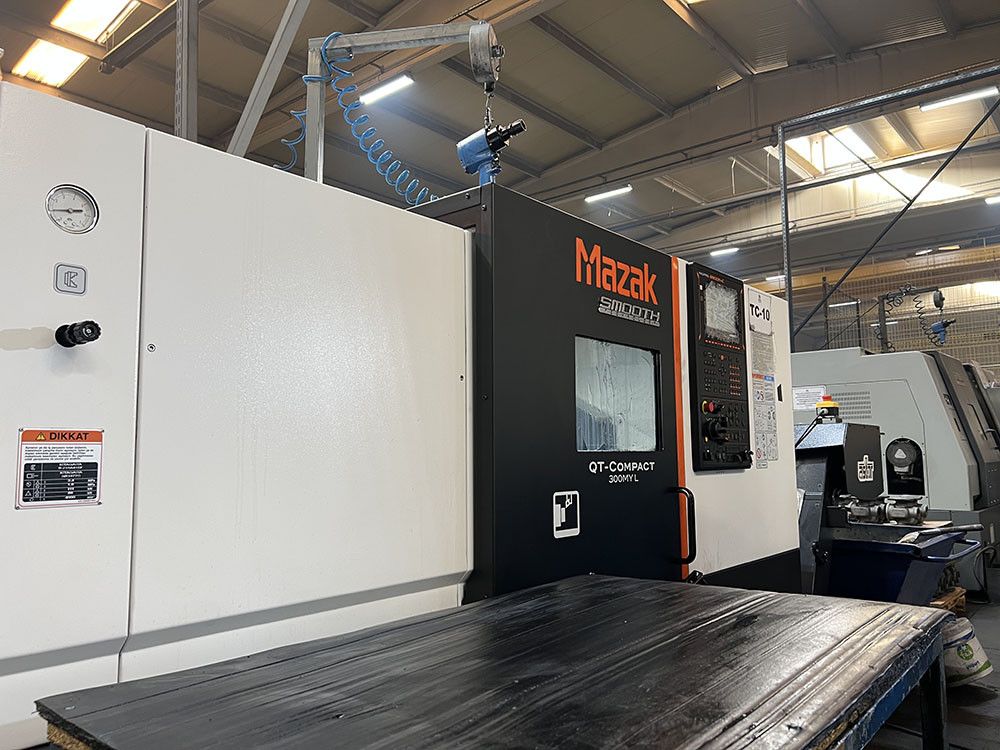
Horizontal and vertical lathes with C and Y axes, vertical machining centres and precision indexing horizontal machining centres.
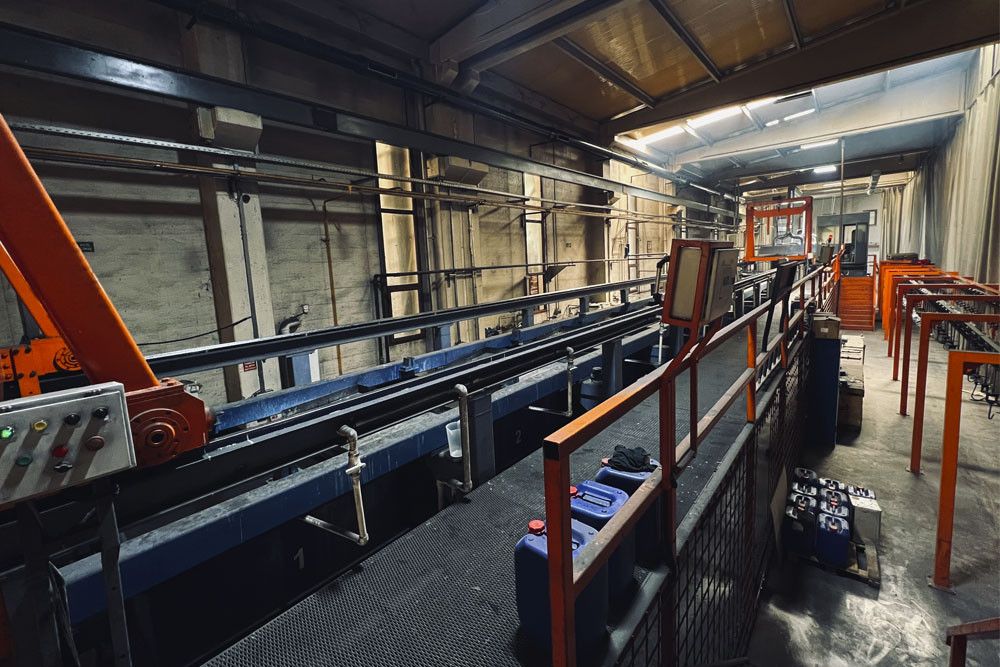
Liquid paint and wet enamel plant for parts of various sizes.
04 — Facility
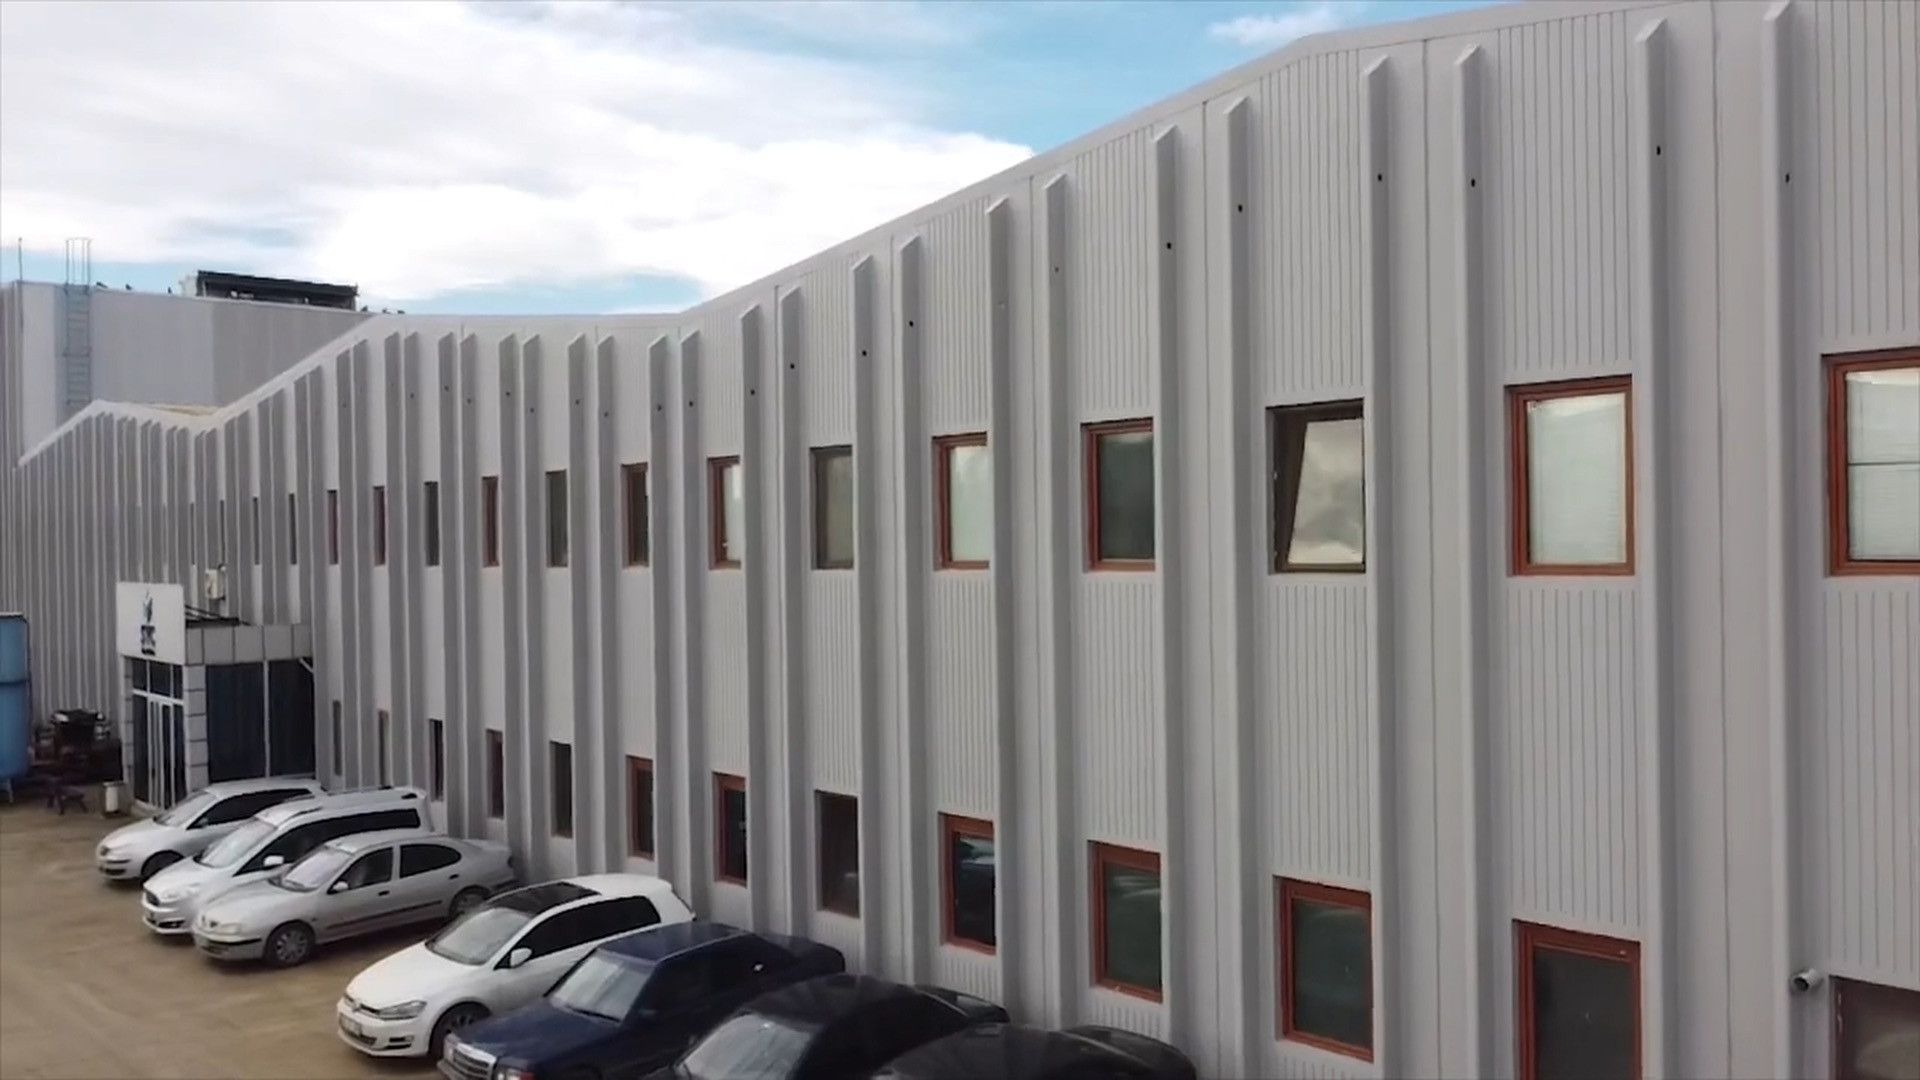
The facility covers a total area of 16,000 m², of which 10,000 m² is covered.
Watch the corporate film (opens in a new tab) When the video starts, a connection to YouTube is made.
05 — Quality
Sand, metallurgical, metallographic, precision dimensional measurement and coating quality checks are carried out.
06 — Industries
07 — Contact
You can start with a drawing or a short description.